 EN
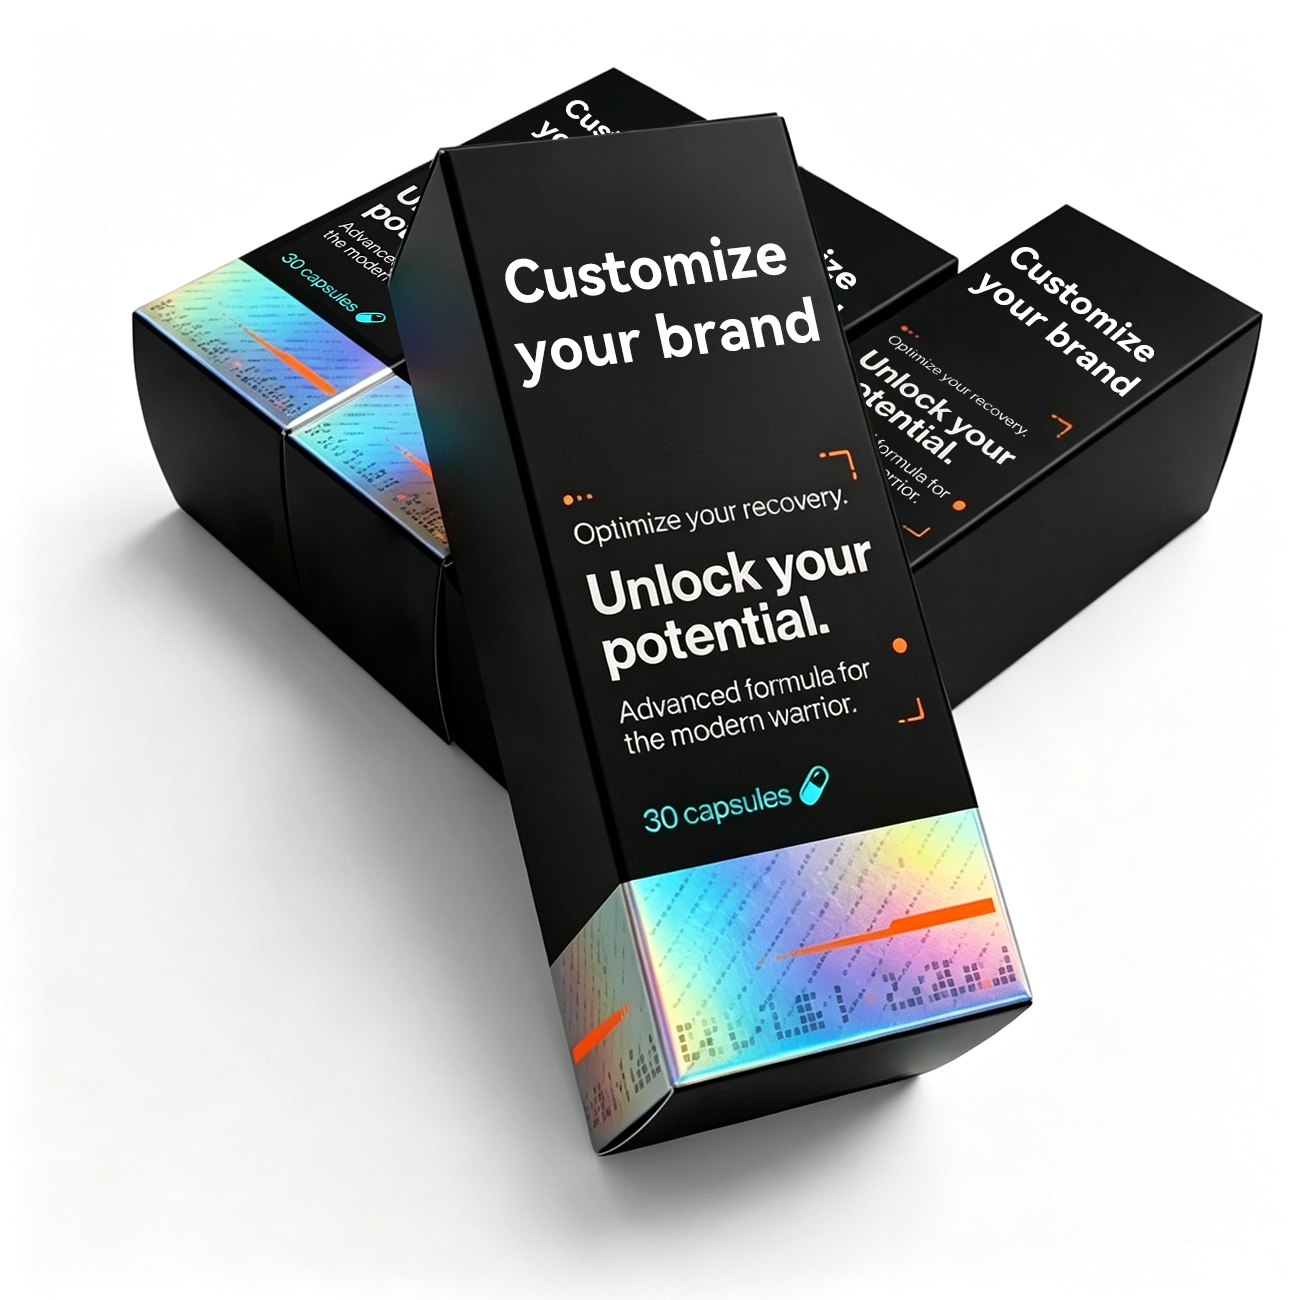
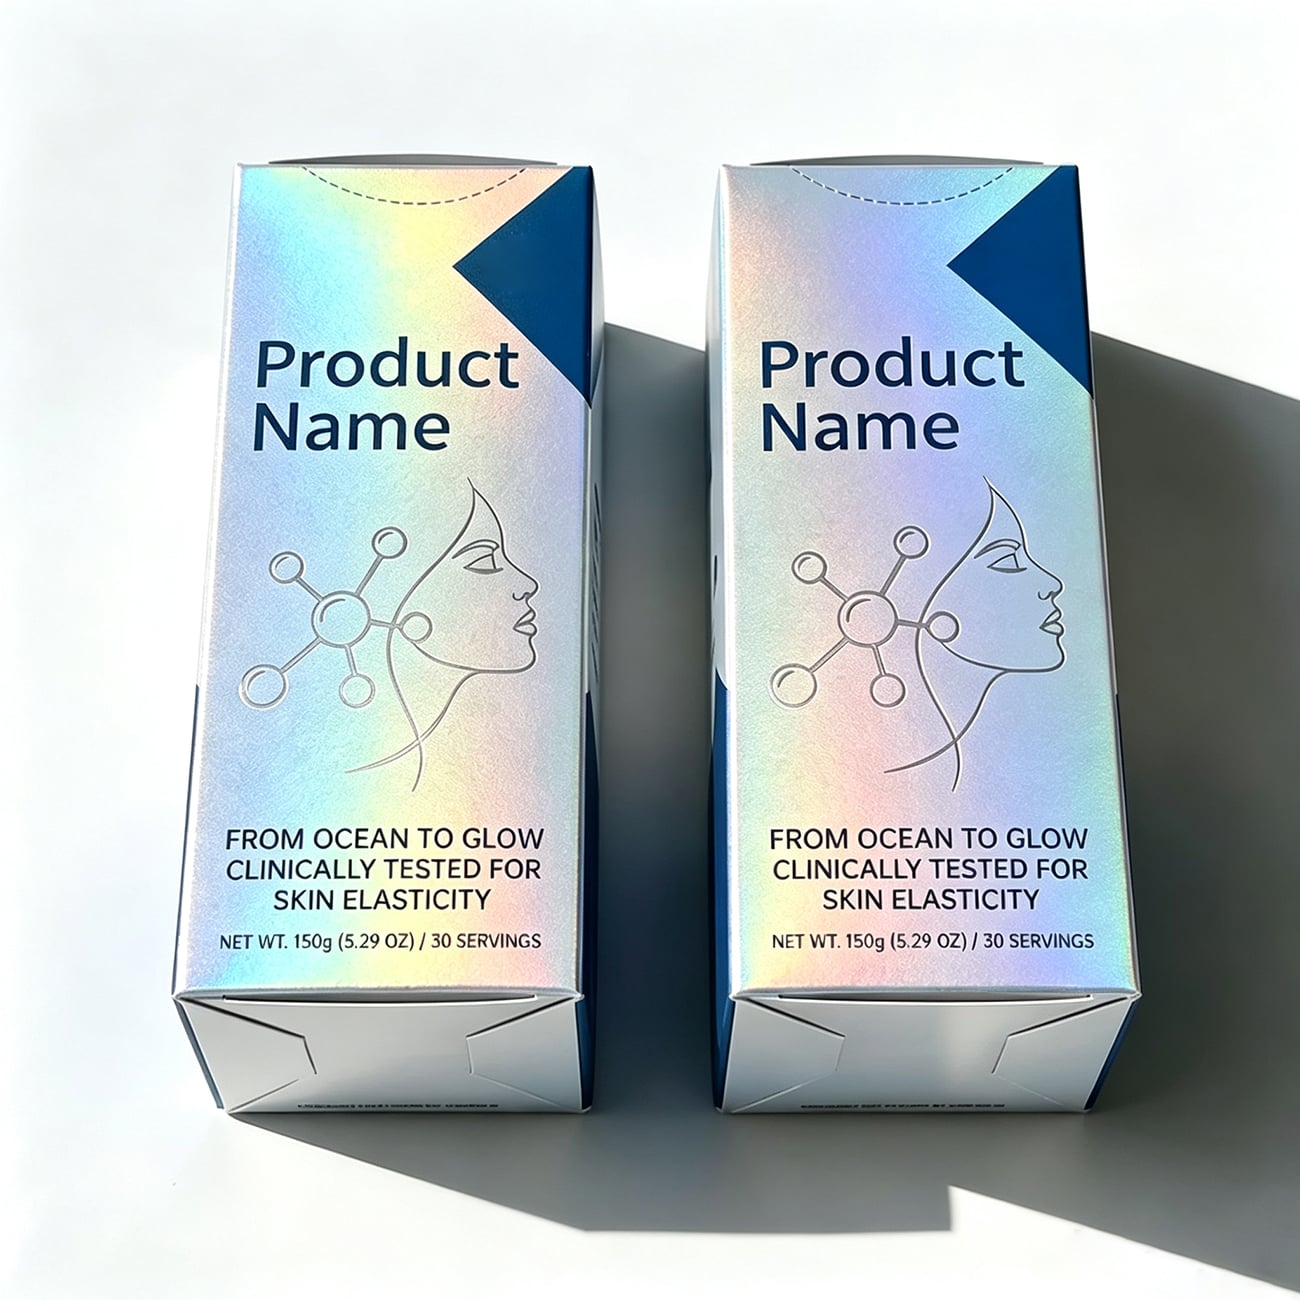
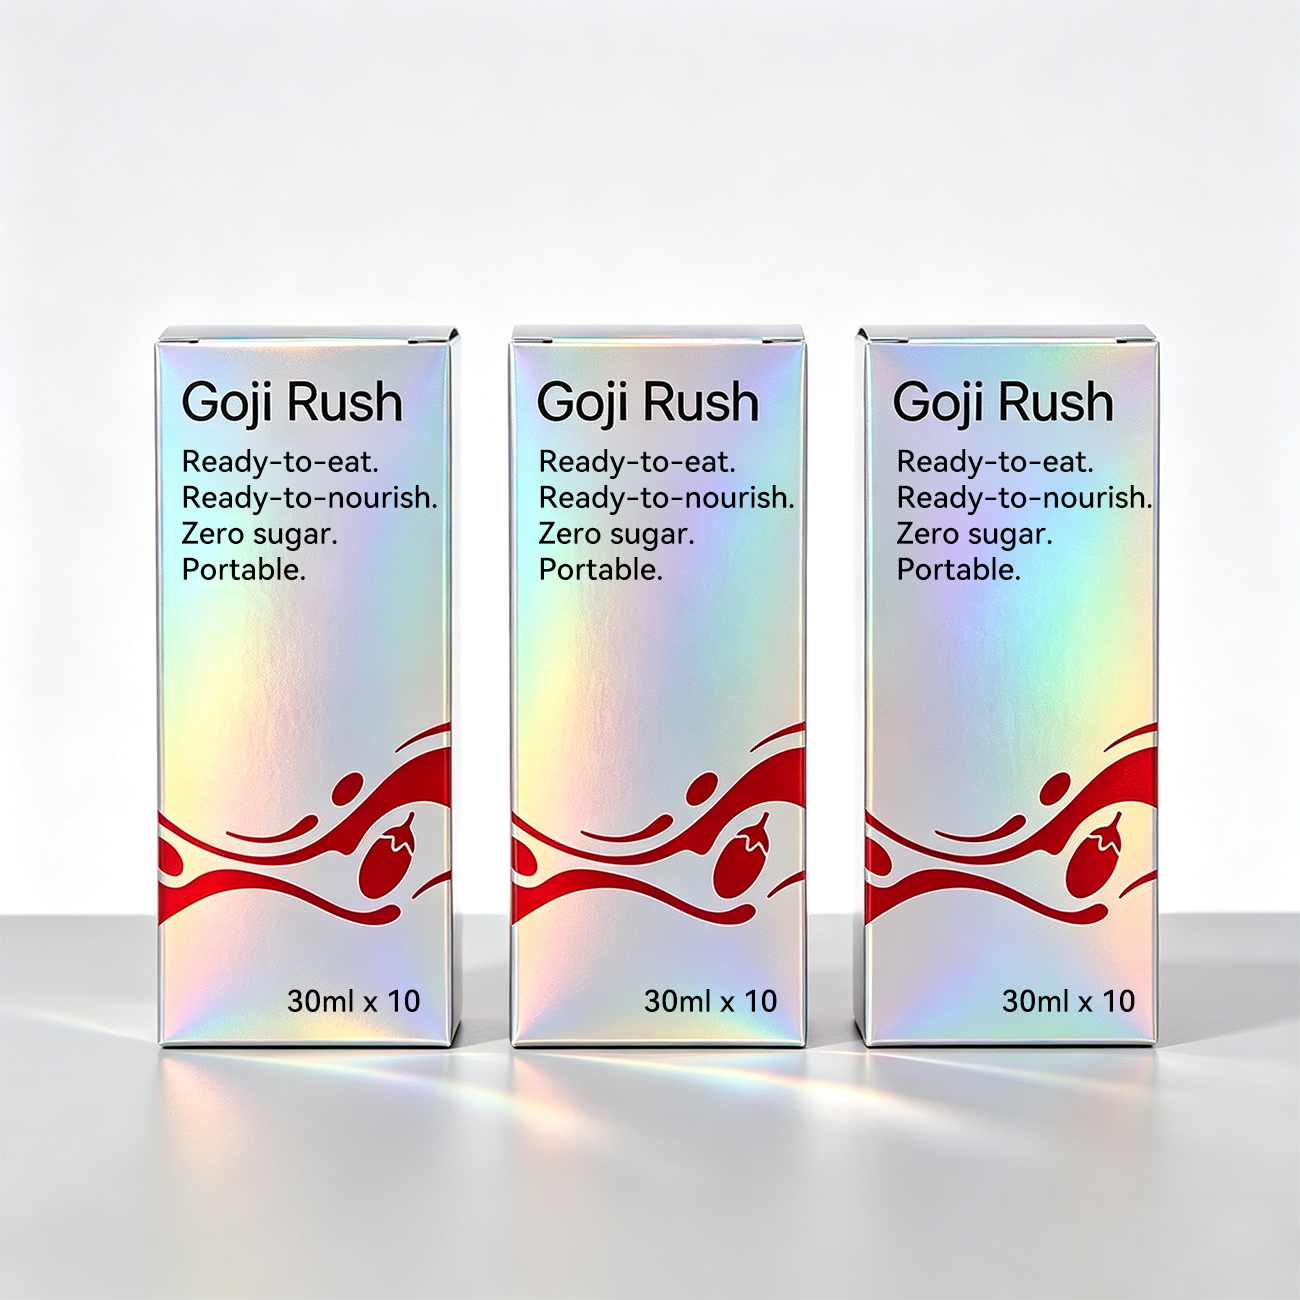
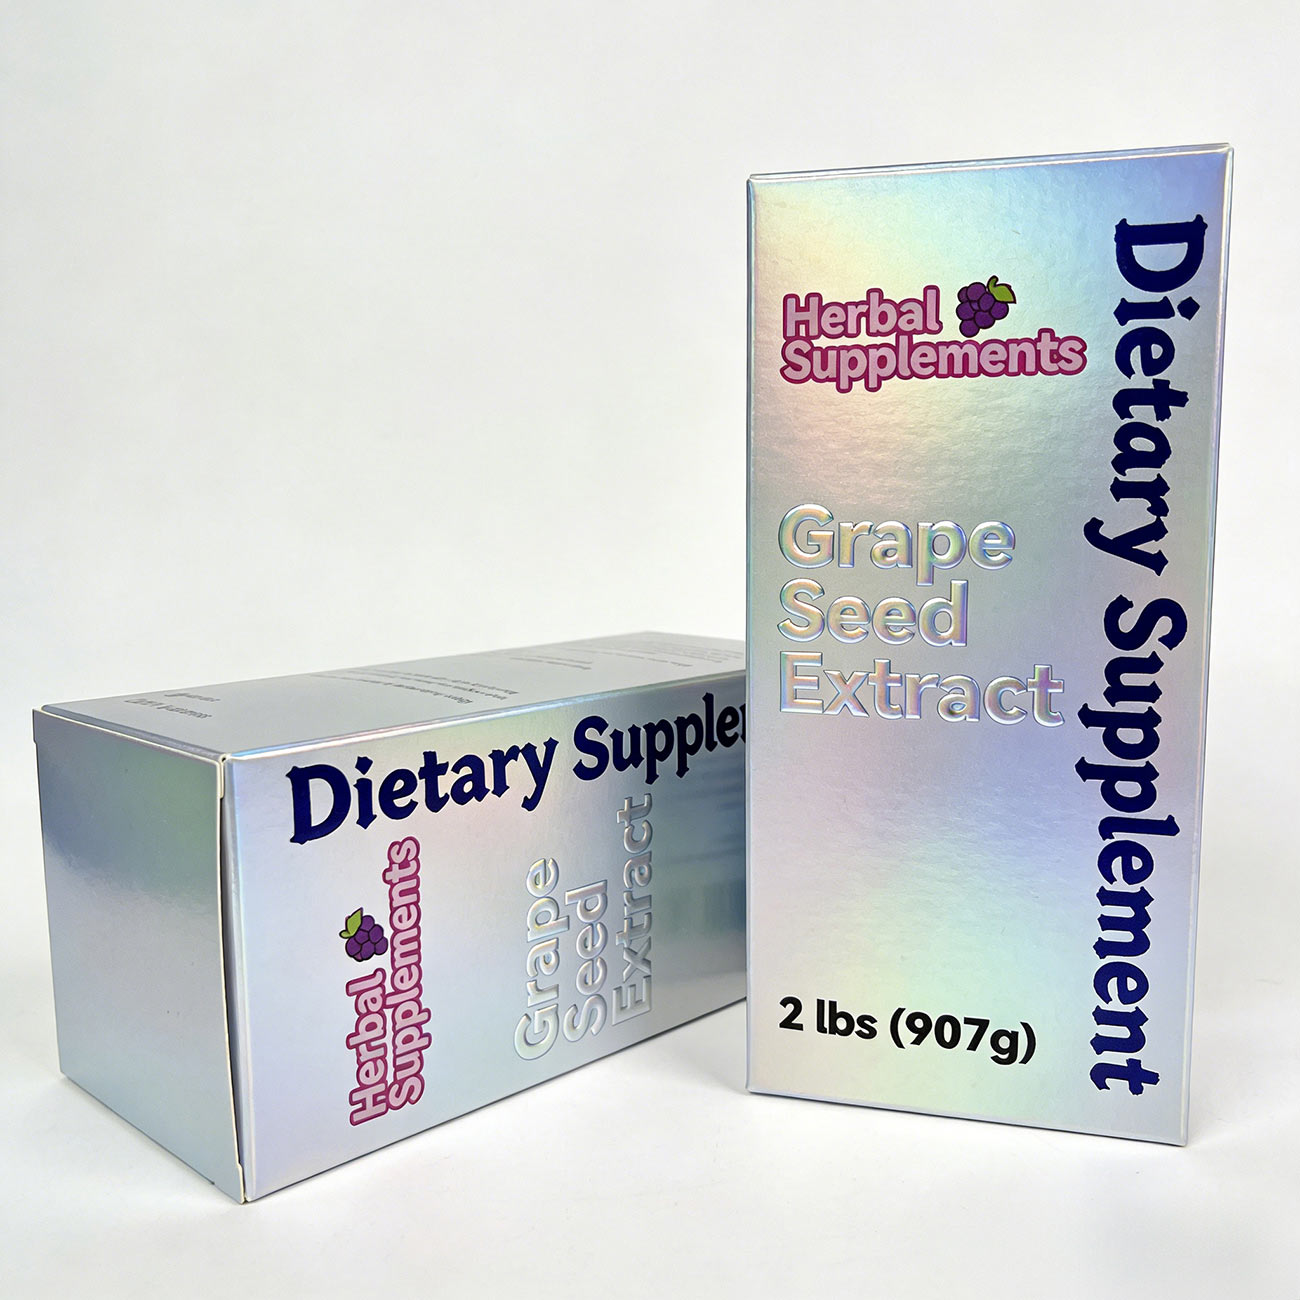
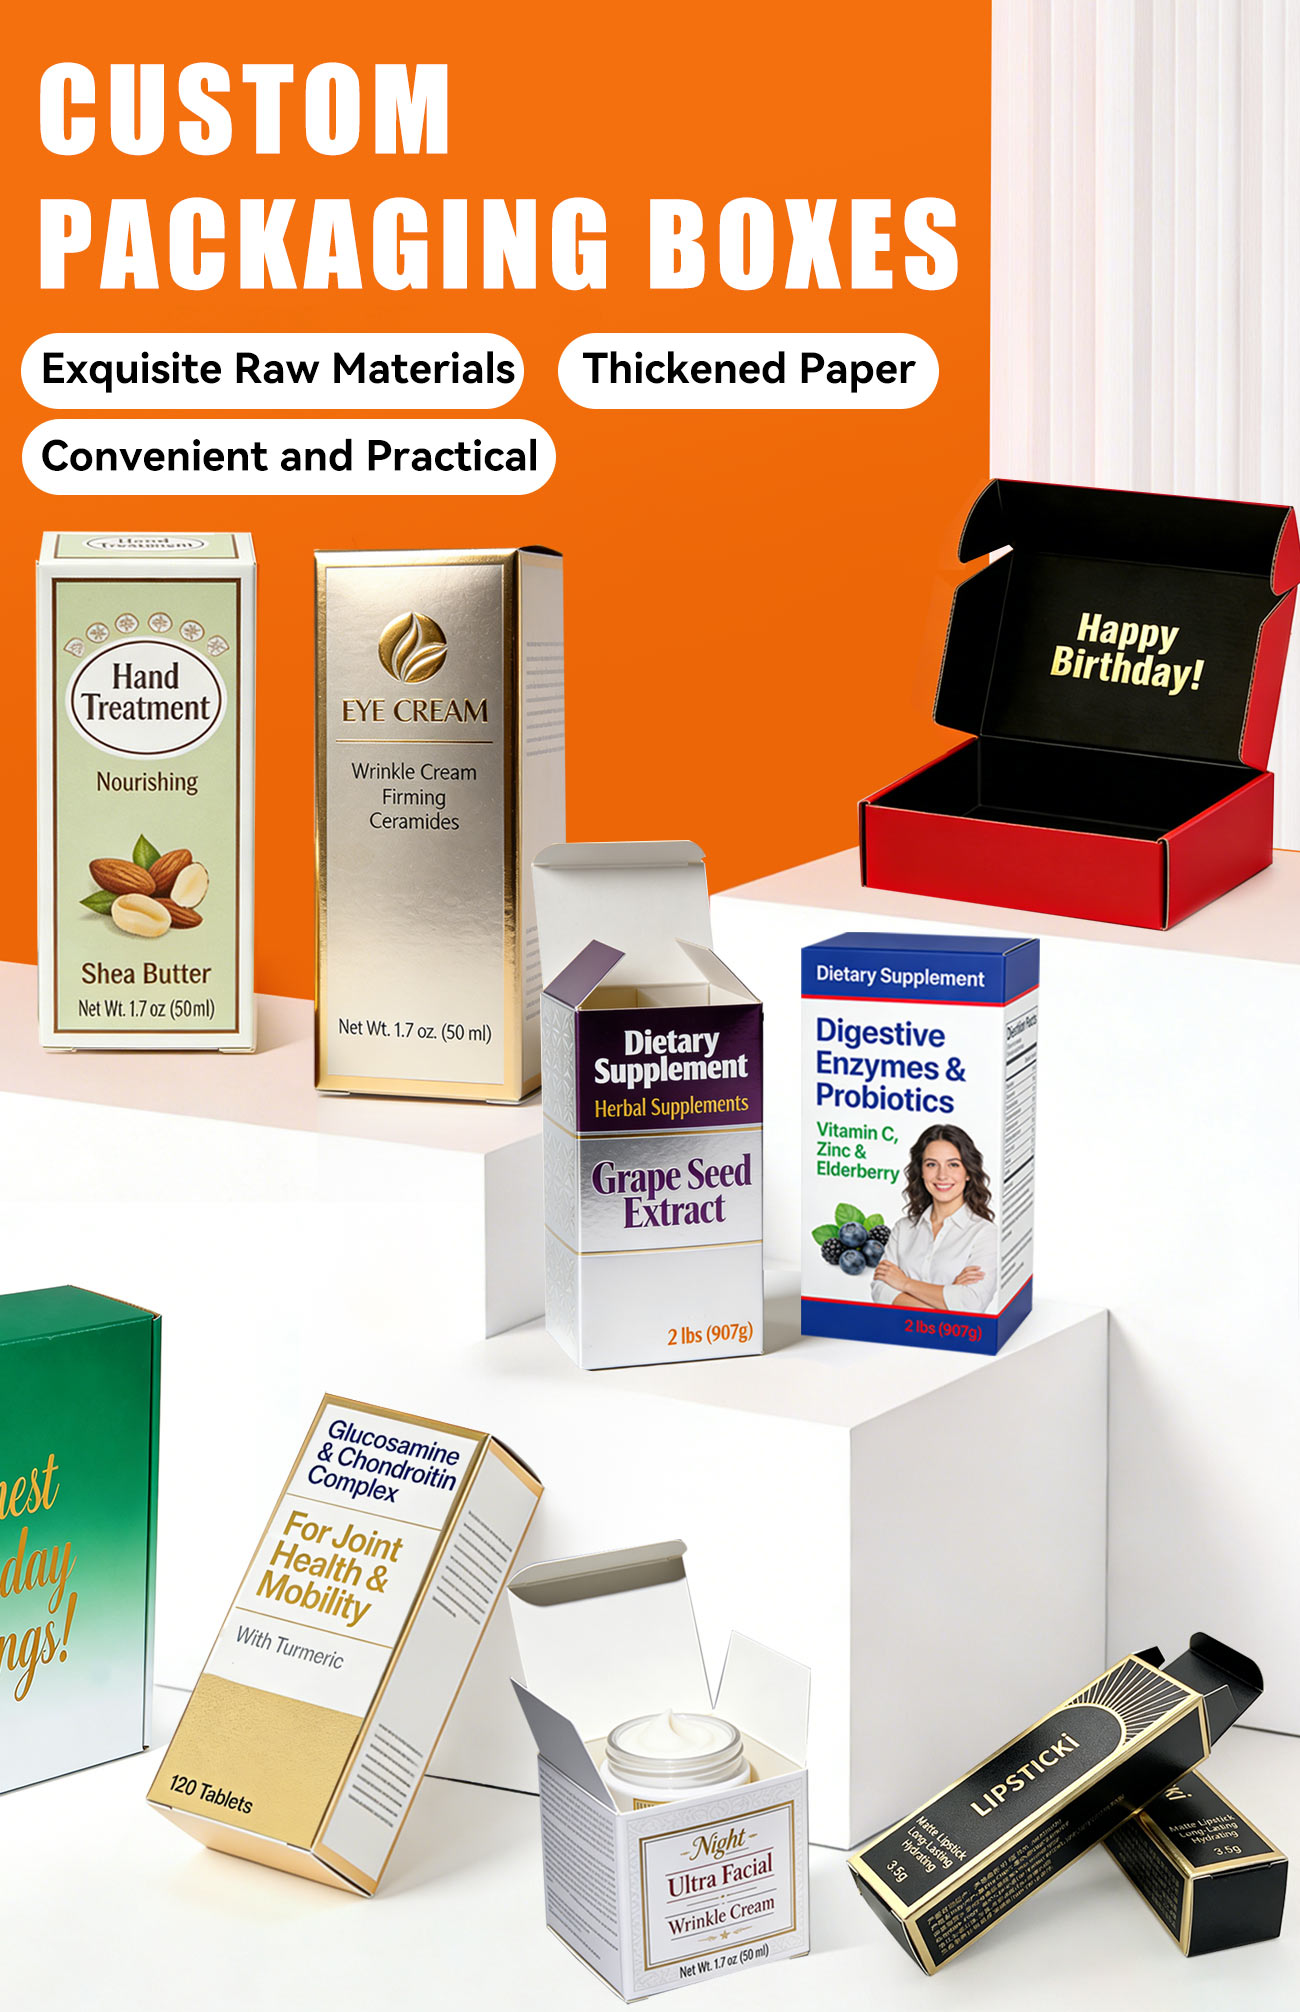
Our custom printed paper boxes are specifically engineered for health supplements, dietary supplements, vitamins, capsules, and functional food brands. As a B2B packaging customization expert, we offer one-stop solutions from structural design and material selection to premium surface finishes. Image 1 showcases a striking contrast between matte black and holographic rainbow effects, while Images 2-4 display the unique metallic luster of full holographic silver cardstock, instantly capturing consumer attention and conveying a sense of technology and premium quality. As a dedicated nutraceutical packaging box supplier, we understand that shelf presence is a decisive factor in a market where dozens of competing products vie for the same consumer attention, and that the right holographic foil carton can transform a standard supplement bottle into a visually arresting retail asset.
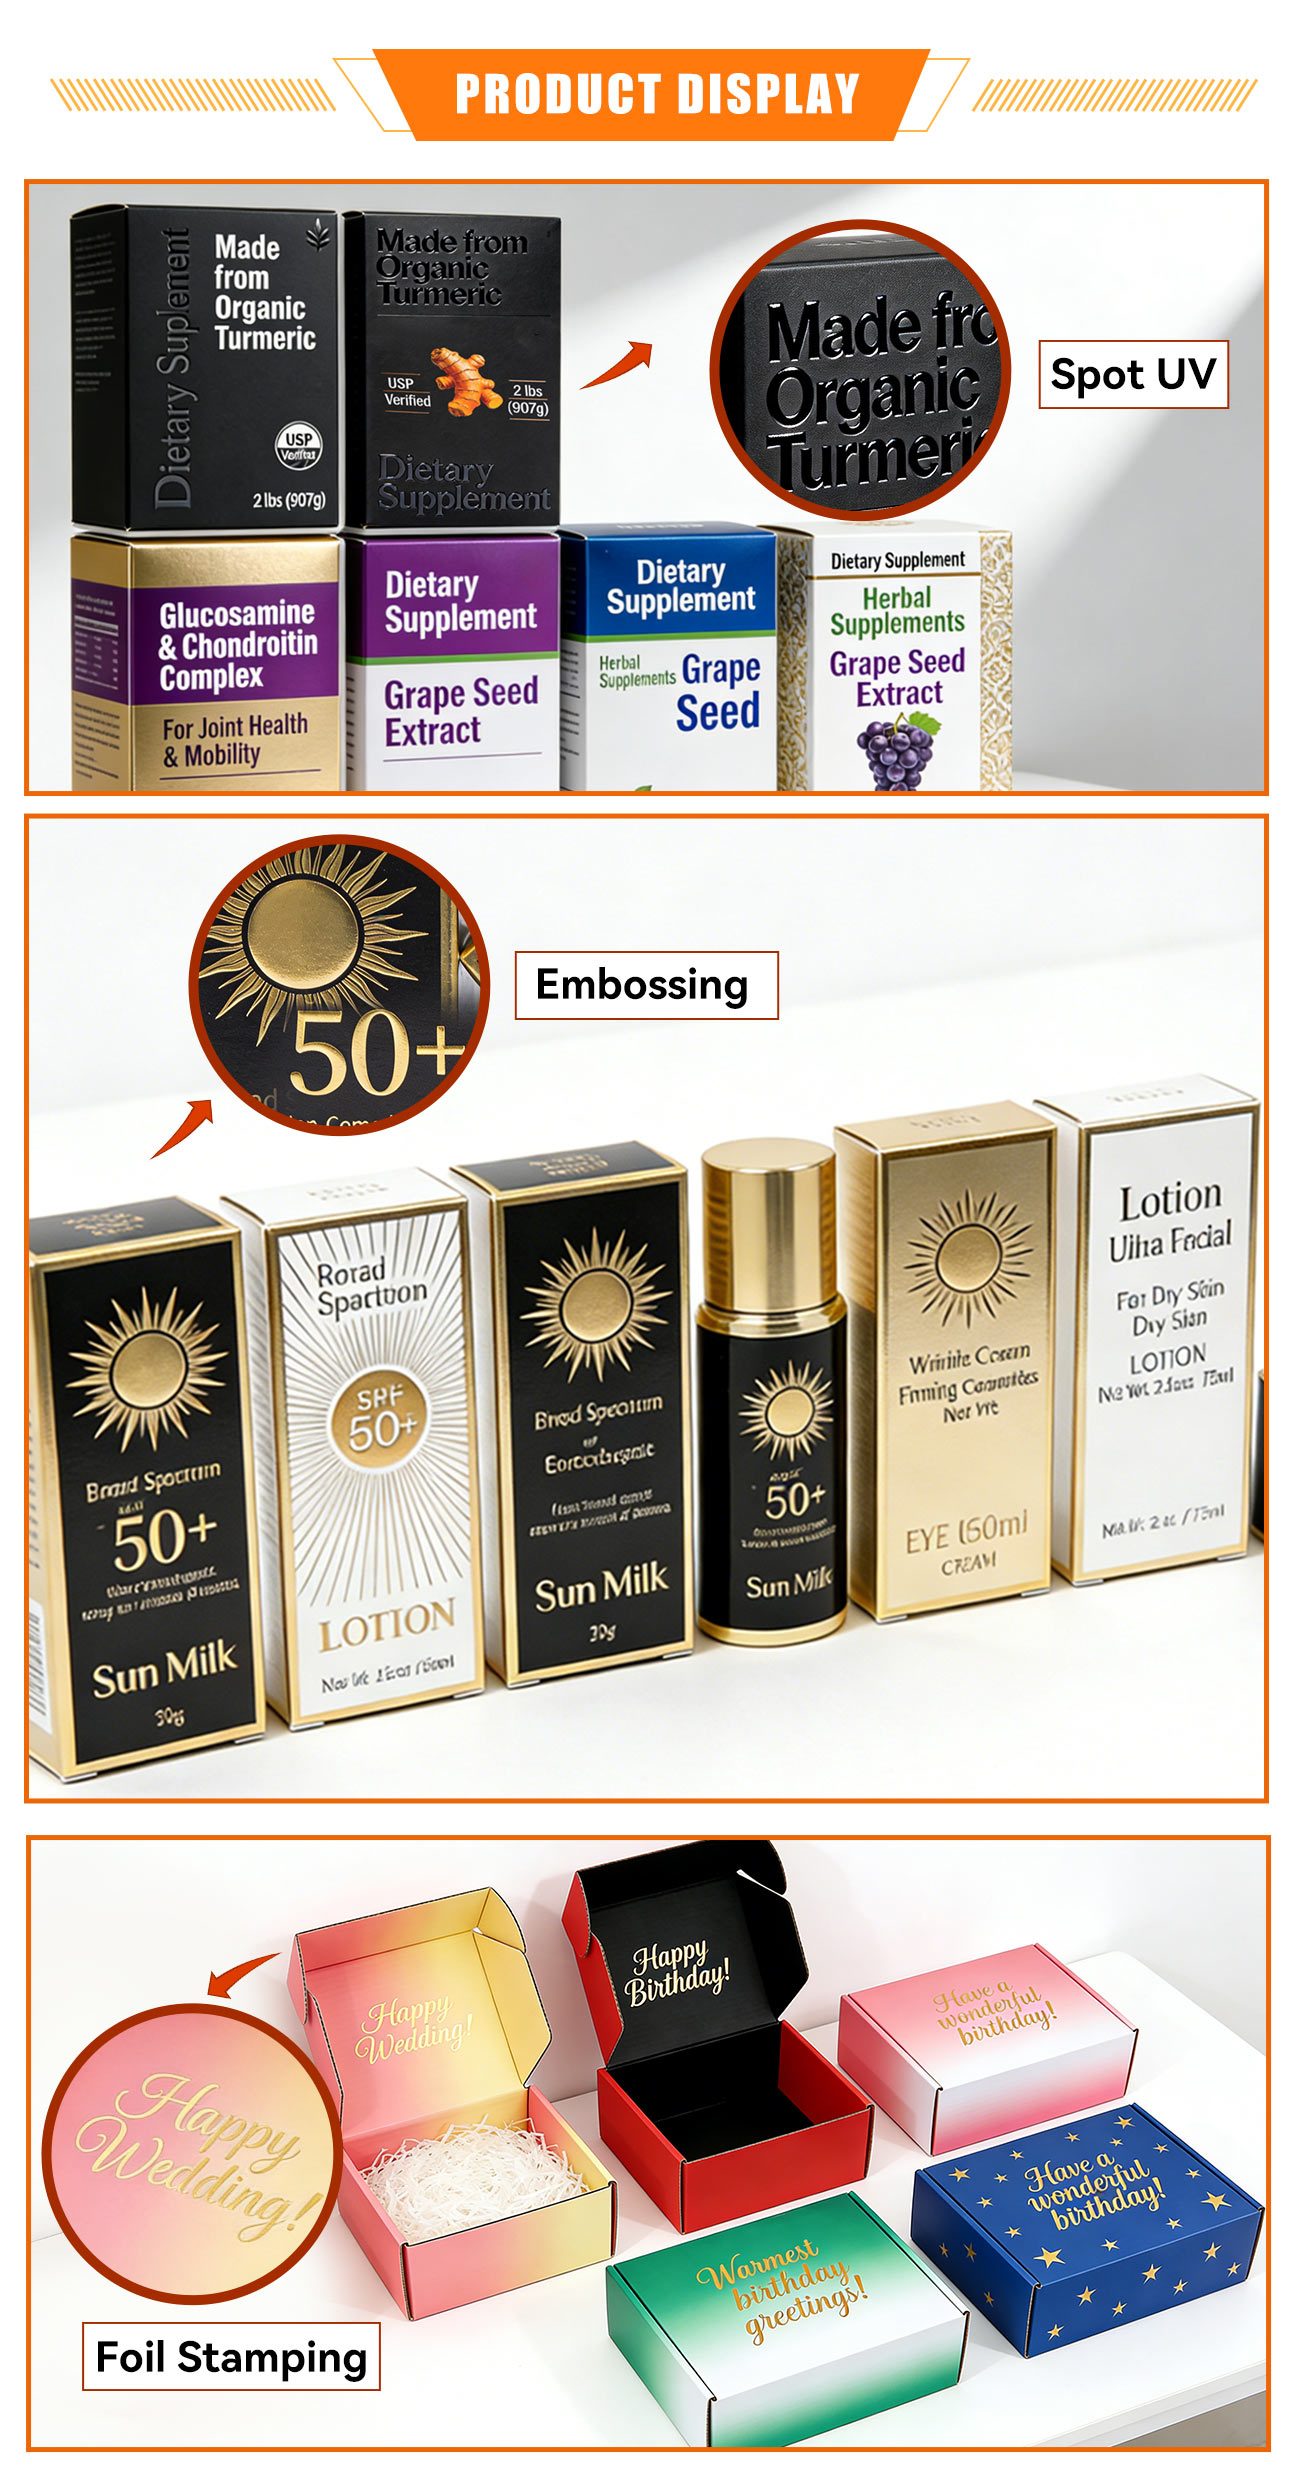
Holographic & Rainbow Effects: Utilizes full holographic silver cardstock or localized holographic transfer technology, displaying rainbow luster under light. Ideal for supplements emphasizing "technology," "rejuvenation," or "purity." The holographic effect is achieved through a transfer process that bonds a metallic layer to the cardstock surface, creating an iridescent finish that shifts in appearance as viewing angles change. The localized holographic transfer option allows brands to apply the effect selectively, highlighting specific graphic elements or brand marks while keeping the rest of the carton surface clean and readable.
High-Definition Printing & Foil Stamping: Supports gold/silver foil stamping, embossing, and spot UV. The "Grape Seed Extract" in Image 4 features 3D silver foil stamping for a premium feel; the orange accents in Image 1 create a sharp contrast against the black background. Foil stamping adds metallic depth and reflectivity that draws the eye under retail lighting, while embossing creates a tactile dimension that reinforces the premium positioning of the brand. Spot UV provides a high-gloss contrast against matte backgrounds, drawing attention to logos, product names, or key claims. The combination of these finishing techniques allows brands to achieve a level of visual and tactile refinement that supports higher price points and stronger shelf differentiation.
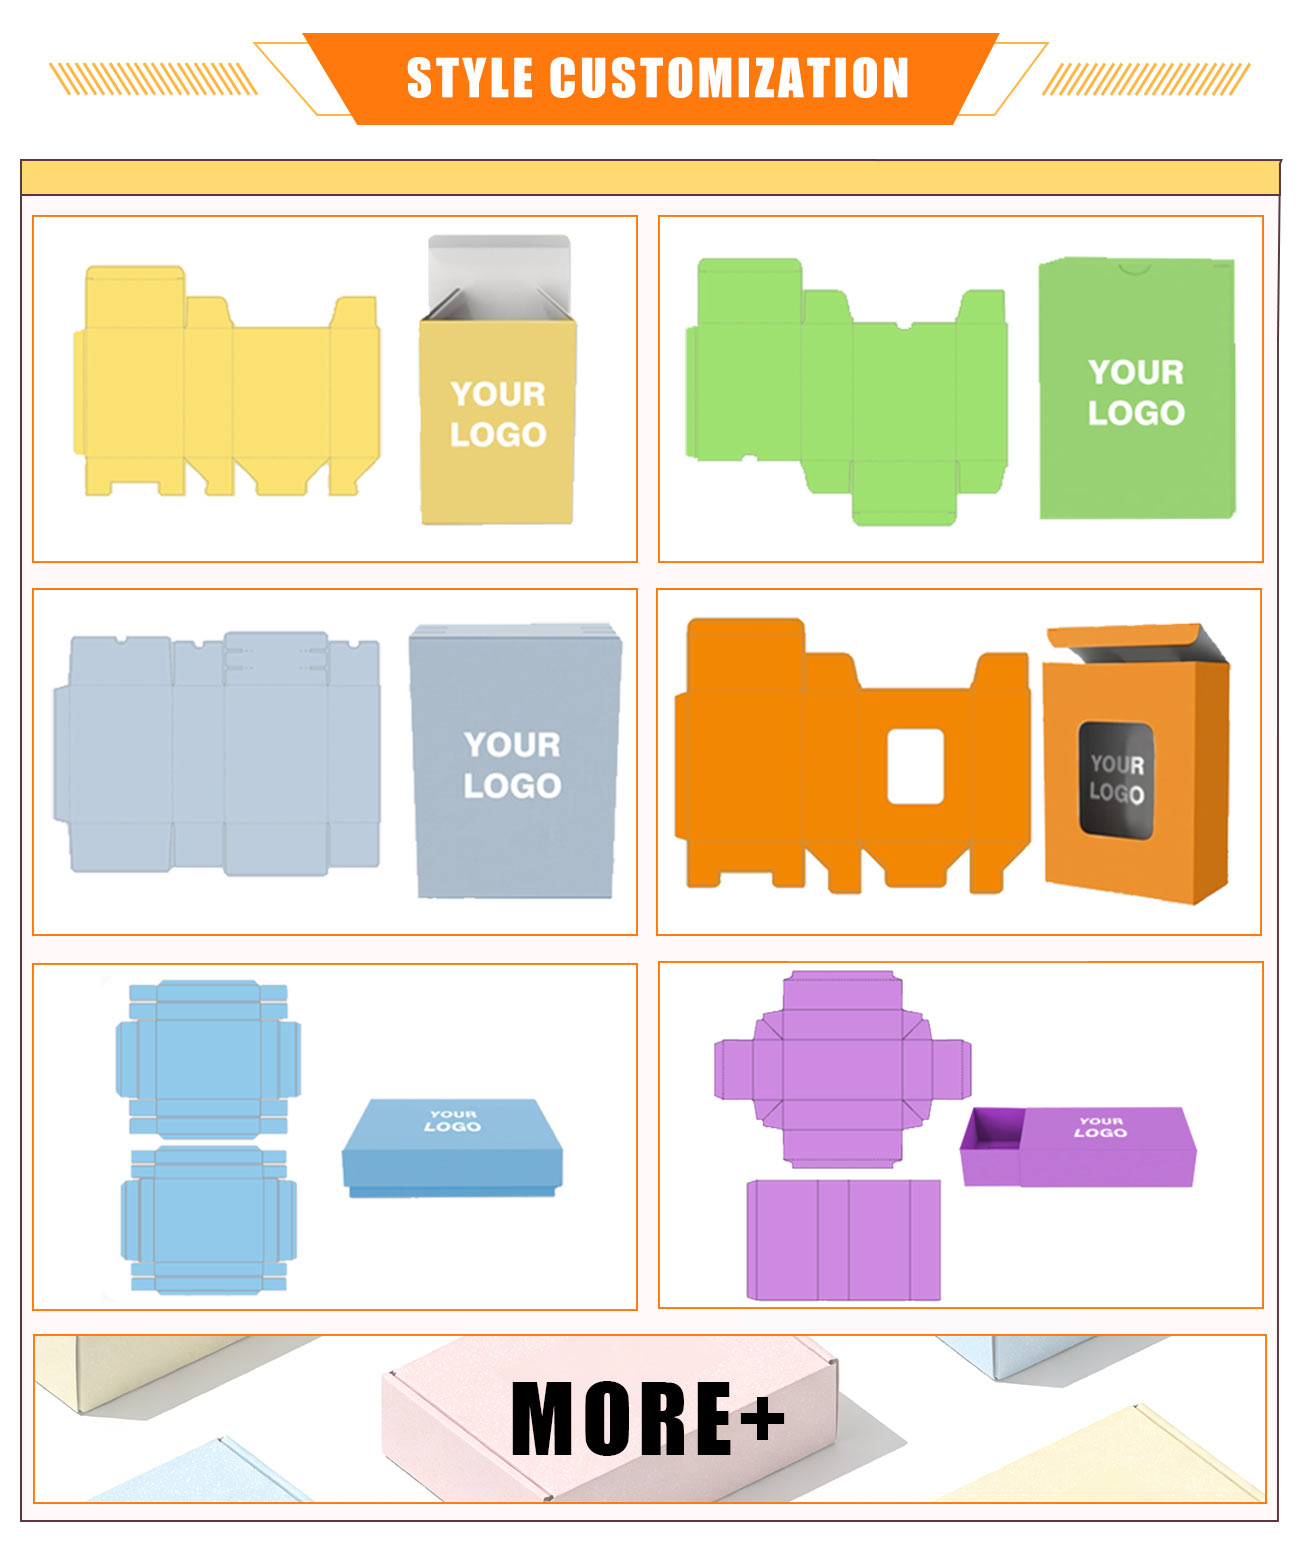
Versatile Box Structures: Supports auto-bottom lock boxes, tuck-end boxes, drawer boxes, etc. Images 2/3 show tear-away perforated designs for easy consumer access. The auto-bottom lock box is particularly suited to high-speed filling lines, as it can be erected quickly and provides a stable base for the product. Tuck-end boxes offer a classic, cost-effective format for smaller cartons, while drawer boxes provide a sliding reveal that enhances the unboxing experience. The tear-away perforated design shown in Images 2/3 allows consumers to open the carton without scissors or excessive force, improving accessibility and reducing frustration at the point of use. This structural versatility makes the custom folding carton supplier relationship valuable for brands with multiple product lines and varying packaging requirements.
Precision Die-Cutting & Folding: High-precision die-cutting ensures smooth folding and excellent formation, suitable for high-speed automatic cartoning machines. The accuracy of the die-cutting process directly affects the performance of the carton on automated filling lines, where even minor dimensional deviations can cause jams or misfeeds. High-precision die-cutting also ensures that the final assembled carton has clean edges, tight corners, and a professional appearance that reflects the quality of the product inside.
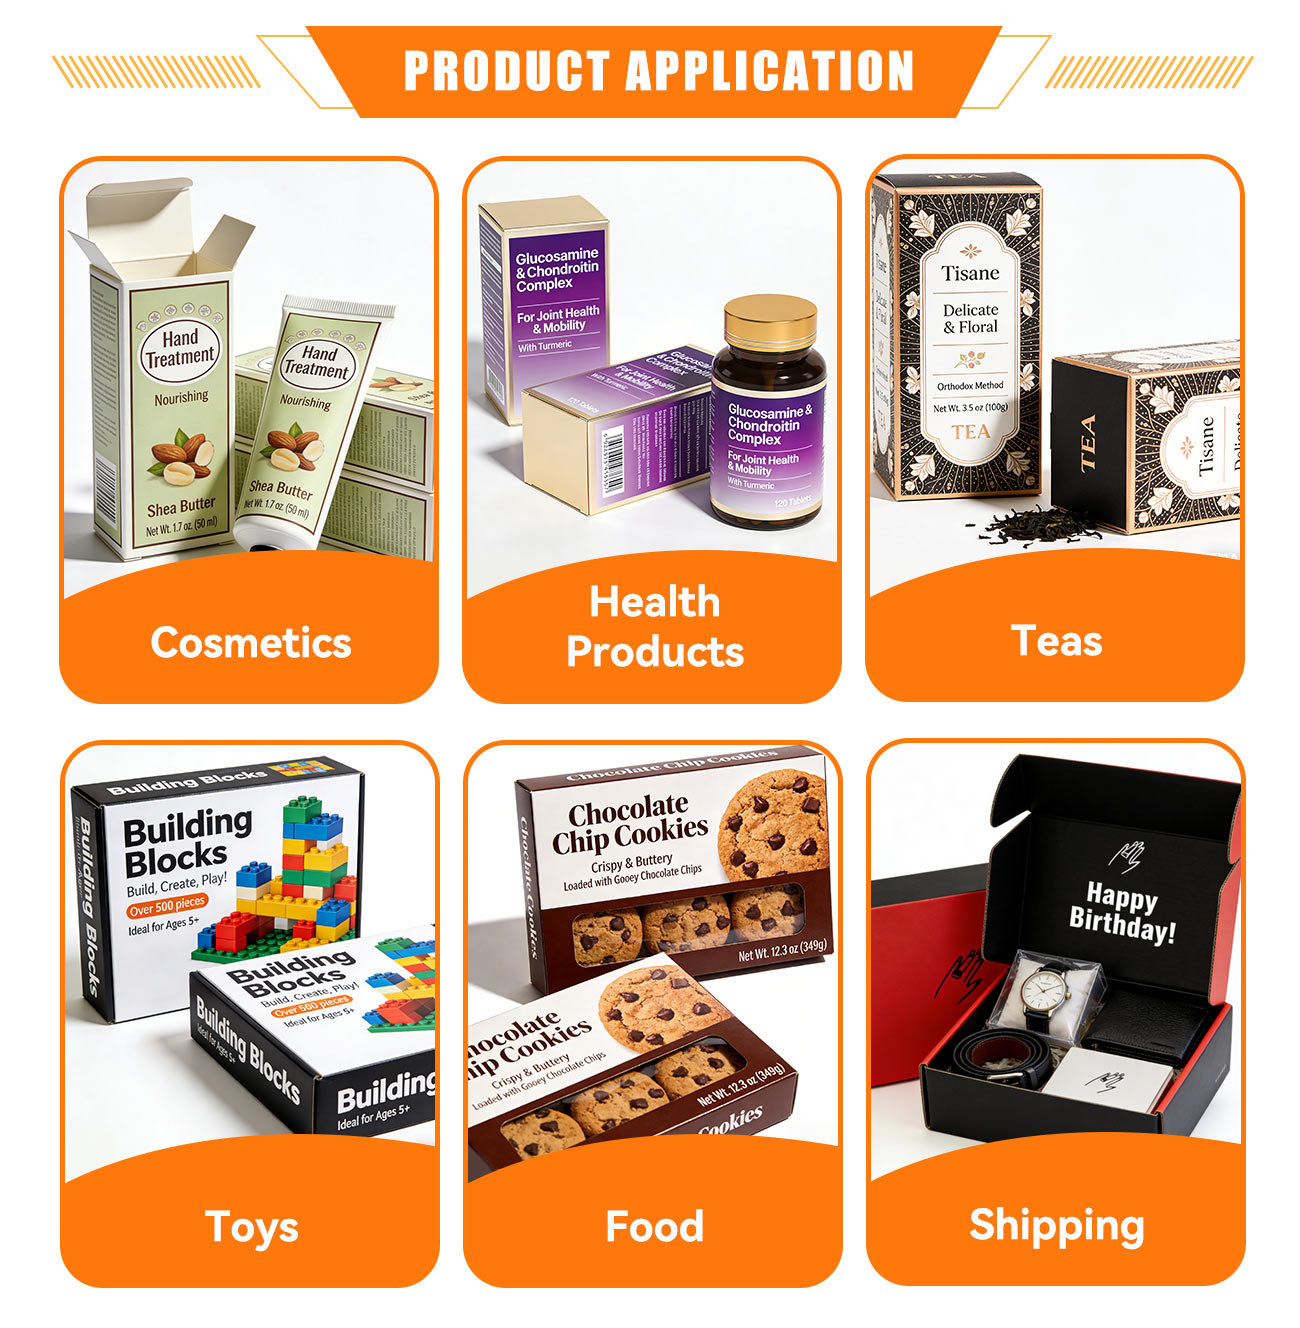
Capsules, tablets, powders, oral liquids, gummies, goji berry juice, grape seed extract, collagen peptides, and other nutraceutical and functional food packaging. The carton format is suitable for both primary and secondary packaging, depending on the product format and retail channel. For bottles and jars, the carton serves as the outer retail package that carries branding, regulatory information, and marketing claims. For blister packs and sachets, the carton provides additional protection and shelf presence. Across all these applications, the nutraceutical packaging box must balance barrier properties, print quality, and structural integrity to protect the product and communicate its value.
Supports small-batch digital printing and large-scale offset/gravure printing. Small-batch digital printing is ideal for new product launches, limited editions, and market testing, allowing brands to validate packaging designs and consumer response without committing to large inventory. Large-scale offset and gravure printing are cost-effective for established products with stable demand, delivering consistent color fidelity and print quality across high-volume runs. This dual capability ensures that brands can scale production as their market presence grows without changing suppliers or compromising on print quality.
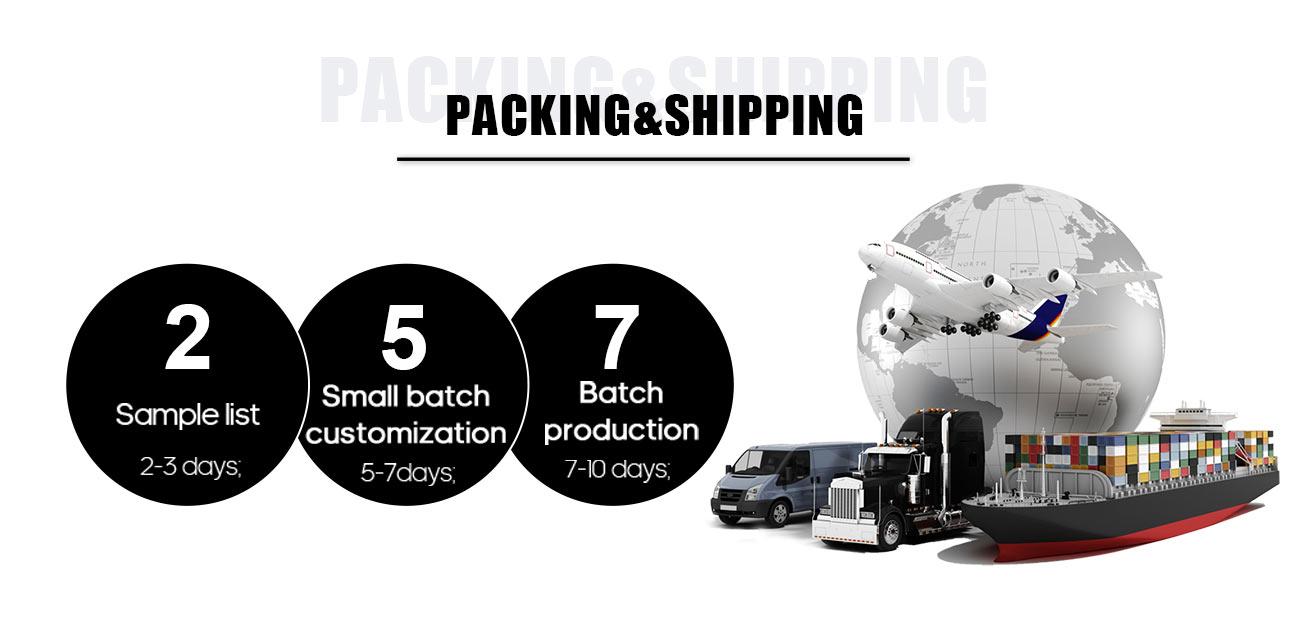
Strict quality control ensures bulk order matches samples. Stable lead times. The quality control process includes material inspection, in-line print checks, die-cutting verification, and final inspection before shipment. This systematic approach ensures that the delivered carton consistently matches the approved sample, reducing the risk of costly rework or returns.
For B2B buyers evaluating packaging investments, the selection of a nutraceutical packaging box involves multiple considerations, including barrier performance, print quality, and total cost of ownership. A holographic foil carton can support premium pricing and shelf differentiation. Brands exploring sustainable supplement packaging options can discuss material alternatives with the technical team to assess compatibility with recycling streams and regional requirements. As a custom folding carton supplier, we work with clients to align packaging specifications with their brand positioning and budget, ensuring that the investment delivers measurable returns.
In summary, our custom printed paper boxes combine holographic visual effects, high-definition printing, and versatile structural options to deliver a packaging solution that helps nutraceutical and functional food brands stand out on the shelf. Whether you need a nutraceutical packaging box, holographic foil carton, sustainable supplement packaging, or a reliable custom folding carton supplier, our team provides the engineering, sampling, and production support needed to bring your packaging vision to life.